
1. When to Use Metal Stamping (and When Not To)
Metal stamping is one of the most cost-effective manufacturing processes for producing high-volume sheet metal components with consistent quality and tight tolerances. However, it is not the right fit for every application. Understanding when metal stamping excels will help you make informed sourcing decisions and avoid costly mistakes.
High Volume Production
Metal stamping excels at high-volume production of 100,000+ parts per year. Progressive dies operating at 1,000+ strokes per minute deliver low per-piece costs and rapid production cycles. Once tooling is complete, stamped parts can be produced faster and cheaper than any other sheet metal process.
Cost at High Volume
Once tooling is built, metal stamping achieves extremely low piece prices at high volumes. The fast 500 to 2,000+ strokes per minute and reusable dies spread fixed costs across large production runs, making per-unit cost highly competitive for volumes above 50,000 annual units.
Consistent Quality
Metal stamped parts exhibit excellent dimensional consistency and repeatability across large production runs. Tight tolerances of plus or minus 0.005 to 0.002 inches are achievable with properly designed dies, reducing scrap and rework costs significantly.
Design Flexibility
Metal stamping accommodates complex geometries including deep draws, bends, holes, and formed features all in a single die press operation. Transfer and four-slide dies enable even more complex designs with multiple forming and assembly operations in sequence.
When to consider other processes
If you need fewer than 10,000 parts annually, metal stamping tooling investment is hard to justify. Laser cutting, waterjet, or small-batch stamping may be more economical. For extremely thick materials exceeding 10mm, forging may be more suitable. For complex 3D shapes requiring extensive hand assembly, investment casting or 3D printing may be better options.
2. Understanding Die Types
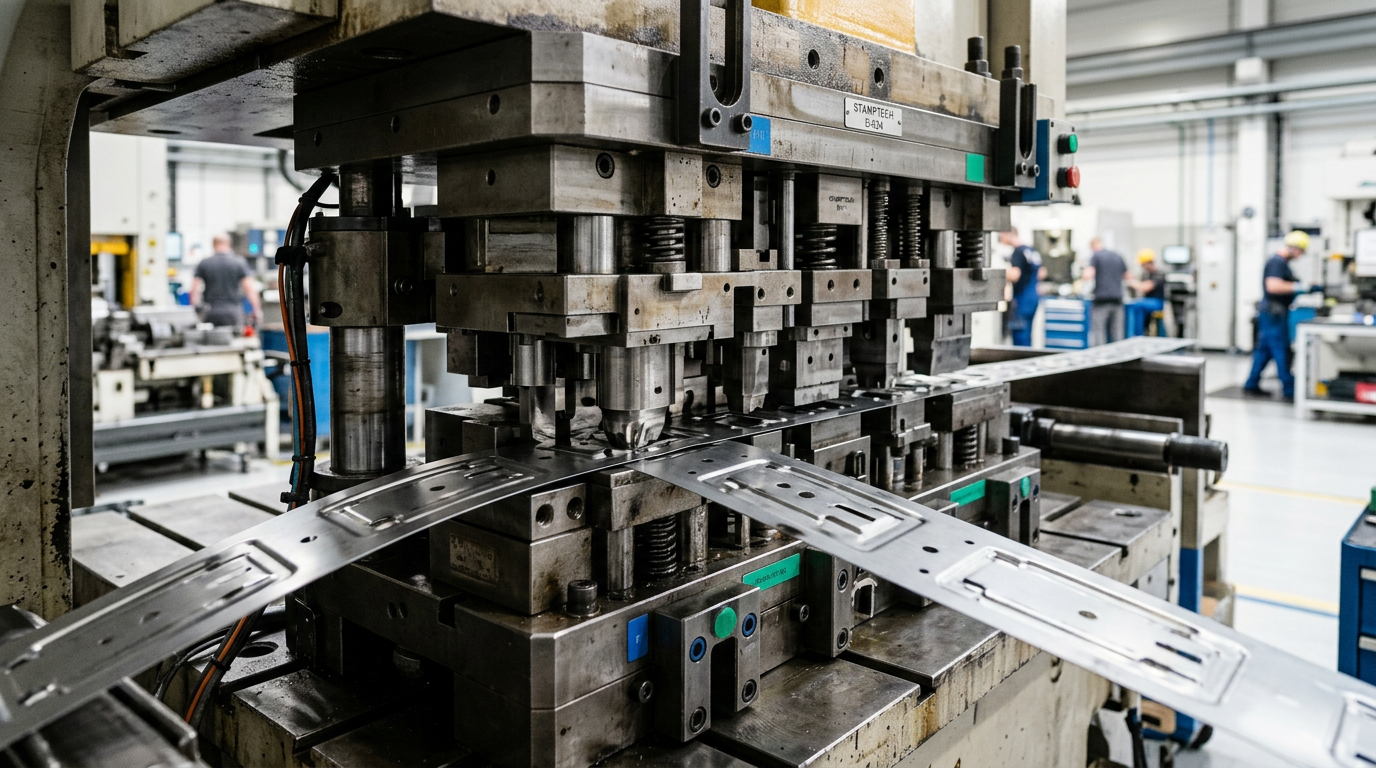
Metal stamping die selection fundamentally shapes your production speed, tooling cost, part quality, and manufacturing flexibility. Understanding the strengths and limitations of each die type helps you select the right approach for your application and volume requirements.
Progressive Dies
A single die with multiple stages that advance the material through each operation in sequence. Ideal for medium to high-volume production of simpler geometries. Operating speeds reach 1,000 to 2,000+ strokes per minute. Each stroke completes multiple operations, reducing cycle time to seconds.
- Speed: 1,000 to 2,000+ strokes per minute
- Best volume: 100,000 to 5M+ parts per year
- Tool life: 500,000 to 2M+ shots typical
- Cost: $30,000 to $100,000+ for production dies
- Best for: High-volume simple to medium complexity parts
Transfer Dies
Multiple separate die stations connected by a transfer mechanism that moves the part between operations. Offers greater flexibility for complex geometries and slower production speeds. Ideal for medium volumes and design-intensive applications requiring multiple forming steps.
- Speed: 100 to 600 strokes per minute typical
- Best volume: 10,000 to 500,000 parts per year
- Tool life: 250,000 to 1M+ shots typical
- Cost: $20,000 to $80,000 per die set
- Best for: Complex multi-operation parts, medium volumes
Four-Slide Dies
Uses four independent slides moving horizontally to perform forming, bending, and assembly operations on a single part. Ideal for complex formed shapes with multiple bends and features. Slower production speeds but eliminates need for secondary assembly operations in many cases.
- Speed: 50 to 300 strokes per minute typical
- Best volume: 1,000 to 100,000 parts per year
- Tool life: 100,000 to 500,000 shots typical
- Cost: $40,000 to $200,000+ for complex assemblies
- Best for: Complex multi-feature formed parts, assembly consolidation
Choosing Your Die Type
Progressive dies deliver the lowest per-piece cost at high volumes but offer less design flexibility. Transfer dies balance cost and complexity for mid-volume applications. Four-slide dies excel at consolidating assembly but run slower. Consult with your stamper early in design to confirm your geometry fits your chosen die type.
- High volume simple: Progressive is most economical
- Medium volume complex: Transfer provides best flexibility
- Lower volume assembled: Four-slide consolidates operations
- Get DFM review early to confirm die type selection
- Changing die type after tooling begins multiplies costs
Pro tip
Engage your metal stamping partner during design phase before tooling decisions are final. A design-for-manufacturability review by experienced stampers catches issues that could require expensive die modifications or prevent use of the most cost-effective die type. Early collaboration saves money and accelerates time to production.
3. Choosing the Right Sheet Metal Material
Material selection dramatically affects part performance, tooling life, production speed, stamping quality, and cost. The most commonly stamped materials represent the best balance of formability, cost, and performance for high-volume production. Here is a guide to sheet metal materials most metal stampers stock:
| Material | Strength | Formability | Best Applications |
|---|---|---|---|
| Mild Steel (ASTM A36) | 36 ksi | Excellent | Most common, cost-effective, automotive, appliances, general fabrication |
| Stainless Steel 304 | 70 ksi | Excellent | Corrosion resistance, food processing, medical, marine environments |
| Stainless Steel 301 | 75 ksi | Excellent | Spring temper applications, clips, fasteners, electrical contacts |
| Aluminum Alloy 3003 | 16 ksi | Good | Weight reduction, electrical applications, requires special dies and process |
| Copper | 30 ksi | Good | Electrical conductivity, decorative applications, higher tool wear |
Pro tip
Mild steel is the default choice for cost-sensitive applications due to excellent formability and widespread availability in all thicknesses and grades. Stainless steel 304 is ideal if corrosion resistance is required. Stainless 301 excels for spring applications. Discuss material selection and available thicknesses with your stamper early, as material availability directly affects tooling design and part cost.
4. Understanding Metal Stamping Tooling Costs
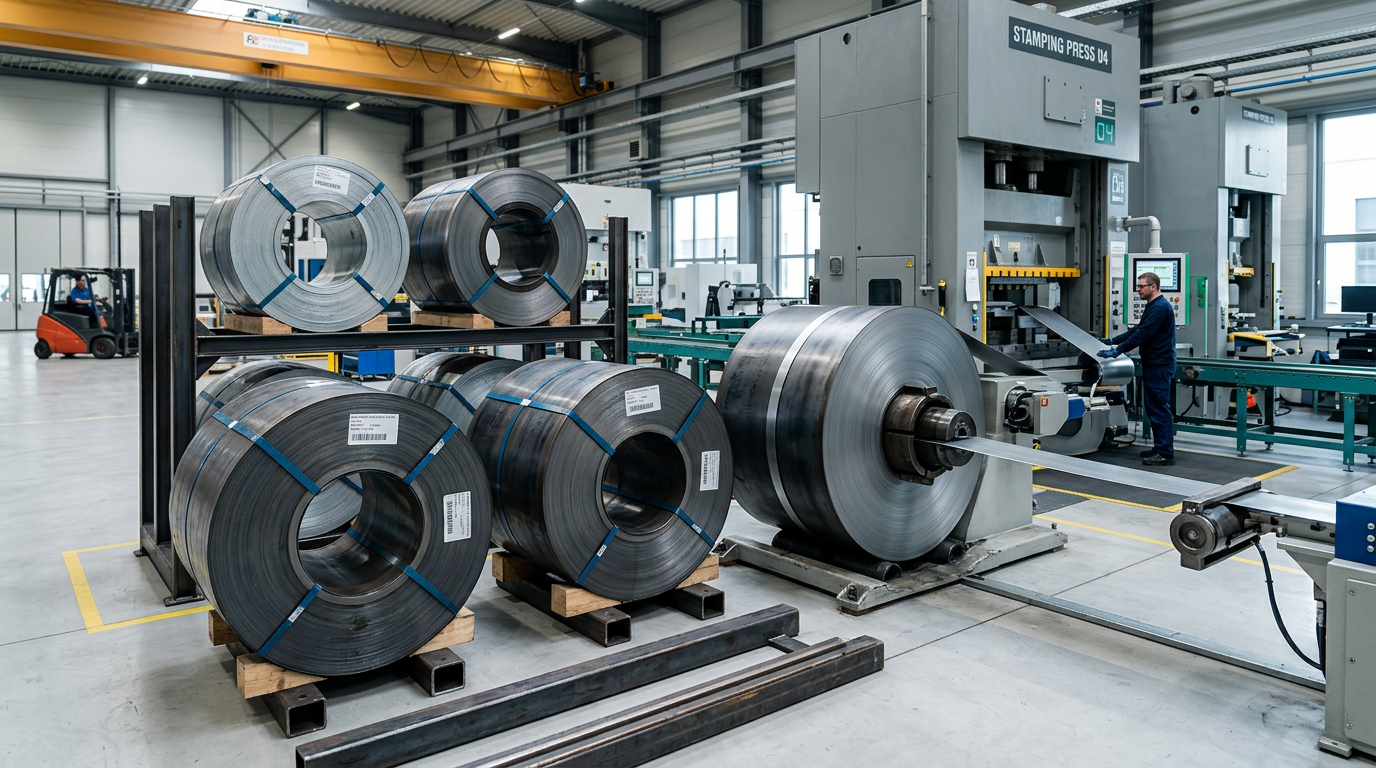
Tooling represents the largest upfront investment in any metal stamping project. Understanding tooling cost drivers helps you budget accurately and evaluate supplier quotes. Metal stamping tooling costs vary dramatically based on die type, part complexity, and production requirements.
Die type and part complexity
Progressive dies for simple stamped parts cost less than transfer dies for complex multi-operation parts. Four-slide dies for assembly-intensive parts cost the most. Number of stations, features per station, and geometric complexity all drive tooling cost upward. Simpler flat stamped shapes cost substantially less than deep-drawn formed parts.
Material and die steel requirements
Hard stainless steel and aluminum stampings require tool steel with higher hardness and toughness, increasing die fabrication cost. Softer mild steel parts use less expensive tool steel and less complex coolant management. Material thickness also affects tool steel selection and die construction difficulty.
Tolerance requirements and secondary operations
Tight tolerances below plus or minus 0.002 inches require precision dies with advanced cooling and dimensional control. Secondary operations like trimming, piercing, or tapping in secondary stations add die complexity and cost. Prototype and tryout dies cost less initially but limit tool life to 10,000 to 50,000 shots.
Press tonnage and die set architecture
Larger parts requiring higher tonnage presses need stronger, heavier die sets. Multi-cavity dies that produce 2, 4, or 8 parts per stroke multiply die machining cost but reduce per-unit production cost significantly. Die set base design, cooling lines, and ejection systems all add to tooling complexity and cost.
| Tooling Type | Cost Range | Best For |
|---|---|---|
| Prototype stamping die | $5,000 to $15,000 | Design validation, 1,000 to 50,000 parts |
| Progressive production die, single cavity | $30,000 to $60,000 | Medium volume production, 100,000 to 500,000 parts |
| Progressive multi-cavity die | $60,000 to $150,000+ | High-volume production, 500,000 to 5M+ annual parts |
| Transfer die set | $20,000 to $80,000 | Complex parts, medium volume, 50,000 to 500,000 parts |
| Four-slide die with assembly | $40,000 to $200,000+ | Complex assemblies, small to medium volume, 5,000 to 100,000 parts |
Watch out
Metal stamping tooling quotes that seem unusually low often indicate shortcuts in die steel quality, inadequate cooling system design, or insufficient machining precision. A poorly designed metal stamping die will experience premature wear, dimensional drift across production runs, and part quality problems. Invest in proper die engineering and proven stamper experience upfront to avoid expensive die modifications during production.
5. How to Evaluate a Metal Stamping Manufacturer
Selecting the right metal stamping partner is as important as die selection itself. A qualified supplier delivers consistent quality, meets aggressive schedules, solves problems proactively, and continuously reduces part costs. Here are the key factors to evaluate when comparing metal stamping manufacturers:
Equipment and Capacity
Do they have press tonnage, speed, and precision capability for your part? What's their maximum part size? How many active press lines? Can they handle your forecasted volume during peak demand? Ask to see the actual equipment, not just spec sheets.
Quality and Certifications
Are they ISO 9001 certified? What quality level do they maintain? Do they have SPC, CMM, and dimensional tracking? Can they provide statistics on scrap rate, rework, and delivery quality? Request recent inspection data for similar parts.
Engineering and DFM
Do they offer design-for-manufacturability reviews? Can they recommend die type, material, and process changes that reduce cost? Do they use CAD and mold flow simulation for complex parts? Early engineering input prevents expensive design errors.
Production Speed and Delivery
What is their typical tooling lead time? Can they meet your production schedule? Do they maintain safety stock of raw material? How do they handle rush orders? What is their on-time delivery record? References from current customers are invaluable.
Secondary Operations
Can they provide finishing services like trimming, tapping, deburring, or painting? Do they have relationships with coating vendors? Can they handle assembly or kitting? Consolidated sourcing simplifies logistics and reduces part cost.
Communication and Support
How quickly do they respond to inquiries? Do you have a dedicated project manager? How do they handle engineering changes and production issues? Regular communication and problem-solving partnerships reduce surprises and build long-term value.
Schedule a facility visit before committing to major tooling investment. A plant tour reveals equipment condition, worker expertise, quality culture, die maintenance practices, and organizational capability far better than any website or brochure ever could.
6. Writing an Effective RFQ
A well-structured RFQ gets you faster responses, better quotes, and more accurate pricing. Include all critical information so suppliers can provide comprehensive cost estimates and timeline projections without multiple follow-up questions:
3D CAD File
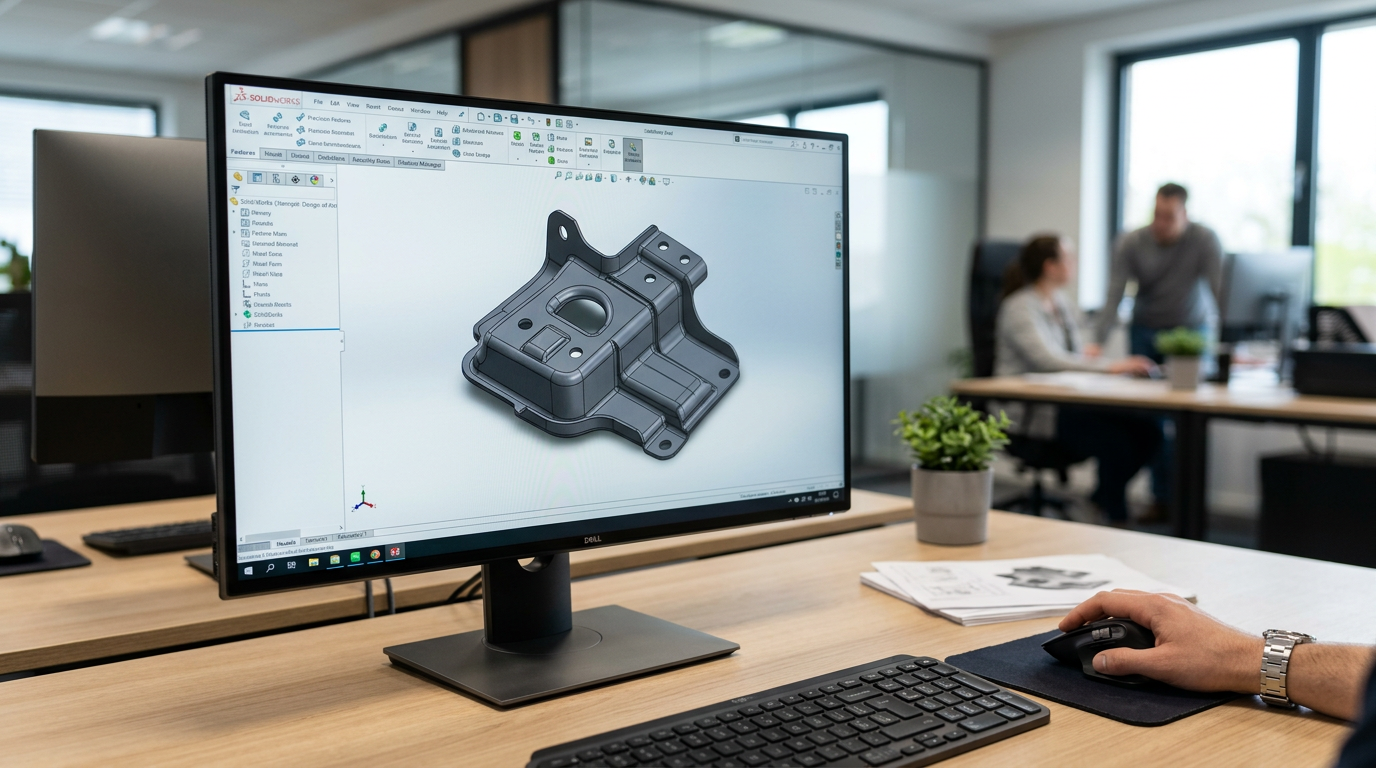
STEP or IGES format with all critical dimensions and features clearly defined
2D Drawing with GD&T
Geometric dimensioning and tolerancing, surface finish callouts, and material specification
Material Requirements
Material grade, thickness, temper condition, and any special certifications needed
Annual Volume
Expected annual quantity and planned release schedule over 3 to 5 years
Secondary Operations
Trimming, tapping, deburring, plating, powder coat, painting, assembly requirements
Quality Standards
Required certifications, inspection level, material testing, and reporting expectations
Pro tip
Send your RFQ to 3 to 5 qualified metal stampers. Fewer than 3 suppliers does not provide sufficient pricing comparison. More than 5 creates noise and dilutes individual supplier attention. Request quotes broken down by tooling cost, per-piece cost at different volumes, and secondary operations so you can compare apples to apples and evaluate total cost of ownership.
7. Common Mistakes Metal Stamping Buyers Make
After years of working with manufacturing buyers, we see the same sourcing mistakes repeated. Learn from these common pitfalls and avoid the costly consequences:
Waiting too long to engage the stamper
Many buyers skip design-for-manufacturability review until tooling quotes arrive. Engaging your stamper early in design phase catches issues that could require $10,000 to $50,000 in die modifications or prevent using the most cost-effective die type. Early consultation saves money and accelerates production.
Choosing die type based solely on initial tooling cost
A cheaper prototype die may seem attractive but limits production to 10,000-50,000 parts before tool failure. Investing in a proper production die upfront costs more but delivers 500,000+ shots and lower per-piece costs. Evaluate total cost of ownership over planned production volume, not just tooling price.
Overspecifying tolerances beyond actual needs
Specifying plus or minus 0.001 inch tolerances when plus or minus 0.005 is sufficient adds significant tooling cost and slows production. Tighter tolerances require precision dies, better equipment, more frequent tool maintenance, and secondary operations. Consult with your designer and end-customer to specify realistic tolerances that balance performance and cost.
Single-sourcing without backup supply
Relying on one metal stamper creates supply chain vulnerability. For critical production parts, develop a qualified second source or ensure your tooling can be transferred to another manufacturer if the primary supplier fails or experiences capacity constraints. Parallel tooling costs more upfront but insures against production disruption.
Ignoring material availability and lead time
Standard materials like mild steel coil are readily available in all thicknesses. Specialized alloys or difficult gauges may have 4 to 8 week lead times. Verify material availability for your thickness and hardness requirements before finalizing design. Material shortages can delay production months after tooling is complete.