
1. When to Use Investment Casting (and When Not To)
Investment casting is one of the most versatile casting processes, capable of producing complex parts in nearly any alloy. But it is not the right fit for every project. Understanding where investment casting excels will save you time, money, and frustration when sourcing.
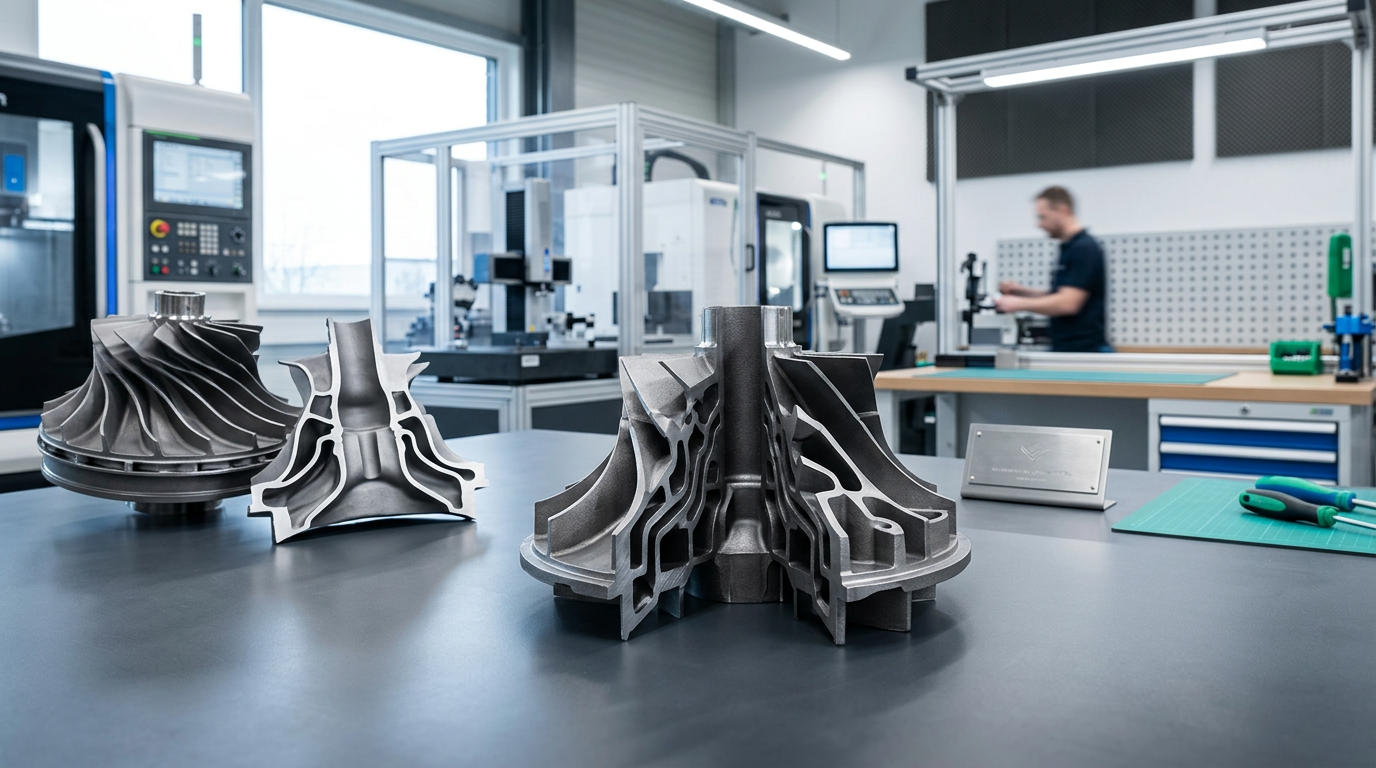
Complex Geometry Freedom
Create intricate internal passages, thin walls, and complex details impossible to machine. Investment casting handles what other processes cannot.
Any Castable Alloy
Stainless steel, carbon steel, superalloys, cobalt chrome, aluminum, bronze, copper. Over 150 alloys available. Use hard-to-machine materials efficiently.
Near-Net-Shape
Produces finished geometry with minimal secondary machining. Reduces material waste and machine time compared to starting from solid stock.
Low to Medium Volume
Cost-effective from prototypes (1 piece) to production runs (100 to 10,000 pieces per year). No massive tooling investment like die casting.
When to consider other processes
For very high volumes (50,000+ pieces per year), die casting may be more economical. For parts under 0.020" wall thickness, investment casting becomes difficult. For rapid iteration, CNC machining from solid stock may be faster initially.
2. The Lost Wax Process: How It Works
Investment casting uses the lost wax method to create incredibly detailed parts. Understanding the process helps you design for manufacturability and set realistic expectations.
Wax Pattern + Shell Building
Inject wax pattern: Molten wax forced into a metal die cavity
Assemble tree: Attach wax patterns to a central wax rod
Build ceramic shell: Dip in silica slurry and stucco, layer by layer
Casting + Finishing
Melt out wax: Heat shell to remove wax, leaving ceramic cavity
Pour metal: Pour molten metal into ceramic shell cavity
Break shell and finish: Remove ceramic, machine, and quality check
Pro tip
Modern investment casters use 3D printed wax patterns for prototypes, eliminating the need for expensive wax injection dies and reducing lead time from 8 to 12 weeks to just 2 to 3 weeks.
3. Choosing the Right Material
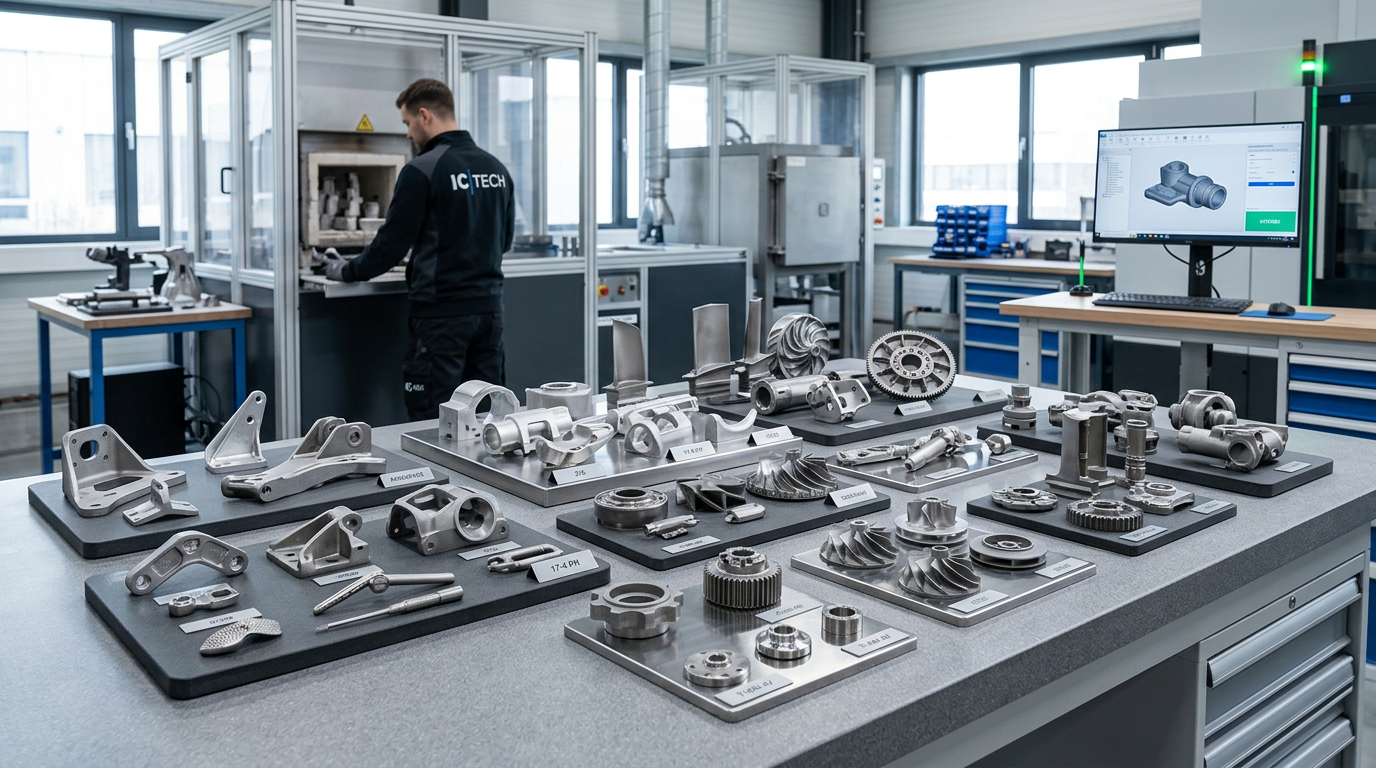
The material you choose affects part performance, cost, and which manufacturers can produce your part. Investment casting offers nearly unlimited alloy options:
| Material | Typical Use | Advantages |
|---|---|---|
| 316L Stainless Steel | Pumps, valves, aerospace | Excellent corrosion resistance |
| 17-4 PH Stainless | Aerospace, high strength | Excellent strength and corrosion |
| Carbon Steel 1045 | General industrial, gears | Good strength, affordable |
| Inconel 718 | Turbine blades, engines | Excellent high-temperature strength |
| Aluminum A356 | Automotive, light parts | Lightweight, good machinability |
| Bronze | Marine, bushings, bearings | Excellent corrosion resistance |
Pro tip
For your first investment casting project, select from common alloys (316L stainless, carbon steel 1045, or aluminum A356). These have established casting parameters and are offered by all major investment casters. Exotic alloys like Inconel or tool steel require specialized expertise and extended lead times, and some shops may decline them entirely.
4. Understanding Investment Casting Tooling Costs
Investment casting tooling costs are significantly lower than die casting, making it economical for small batches. Understanding cost drivers helps you budget accurately and identify the most cost-effective path for your application.
Wax injection die design and complexity
Simple cavity wax dies cost less than dies with internal passages, undercuts, or slides. Die cost depends on cavity count (single versus multi-cavity) and whether cores are needed inside the wax pattern.
3D printed wax patterns for prototypes
Avoid wax injection dies entirely using 3D printed wax patterns. Ideal for prototypes, low-volume runs (under 100 parts), and design validation without any tooling investment.
Part size and shell building costs
Larger parts require thicker ceramic shells and more material. Multiple dipping cycles add labor cost. Part size directly affects ceramic shell cost and casting cycle time.
Alloy and thermal processing
Exotic alloys (Inconel, tool steel, cobalt chrome) require specialized melting equipment and inert atmosphere furnaces, increasing per-part cost. Standard alloys (stainless 316L, aluminum A356, carbon steel) are most economical.
| Tooling Type | Cost Range | Best For |
|---|---|---|
| 3D printed wax pattern | $1,000 to $5,000 | Prototypes, design validation, low volume (1-25 parts) |
| Wax injection die, single cavity | $5,000 to $25,000 | Small production runs (50-500 parts per year) |
| Wax injection die, multi-cavity | $25,000 to $50,000+ | Medium to high volume (1,000-10,000+ parts per year) |
Watch out
Investment casting tooling quotes that seem unusually low often indicate shortcuts in wax die quality, inadequate shell dipping cycles, or non-optimized gating. Underbuilt tooling leads to defects, scrap, and expensive rework. Request references and ask about their average first-article scrap rate (should be under 5%).
5. How to Evaluate an Investment Casting Manufacturer
Use this comprehensive evaluation framework to confidently select an investment casting supplier that meets your technical requirements, quality standards, and business needs:
Furnace Capacity
What alloys can they melt? Do they have vacuum furnaces for superalloys? Induction melting for stainless? Can they handle your required material?
Quality Certs
ISO 9001 is essential. IATF 16949 required for automotive. AS9100 for aerospace. What inspection equipment (CMM, spectrometer, X-ray)?
Part Size Limits
What is their maximum part weight? Can they handle your part size and weight? How does part size affect lead time and cost per piece?
Lead Times
How long from RFQ to first article? From tooling completion to production? Can they accommodate rush orders? What is typical delivery frequency?
Engineering Support
Do they offer design-for-manufacturability review? Can they suggest gating, cooling, or alloy changes? Are their engineers responsive to design questions?
Communication
How quickly do they respond to inquiries? Do you have a dedicated account manager? How do they handle engineering changes?
If possible, visit the facility before committing to a major tooling investment. A plant tour tells you more about a manufacturer's capabilities, quality systems, and ability to handle your specifications than any brochure or website can.
6. Writing an Effective Investment Casting RFQ
A well-written RFQ gets you better quotes, faster responses, and more accurate pricing. Here is what to include:
3D CAD File
STEP or IGES format with all critical dimensions called out
2D Drawing with GD&T
Tolerances, surface finish requirements, and material callout
Material Specification
Alloy grade and any special requirements
Annual Volume
Expected order quantities per release
Secondary Operations
Machining, finishing, assembly, testing needs
Quality Requirements
Certifications, inspection level, and reporting needs
Pro tip
Send your RFQ to 3 to 5 qualified investment casters. Fewer than 3 does not give enough pricing comparison. More than 5 creates noise and dilutes each supplier's attention. Browse our investment casting manufacturer directory to find qualified suppliers.
7. Common Mistakes Buyers Make
After working with hundreds of manufacturing buyers, we see the same sourcing mistakes come up repeatedly. Avoid these and you will save significant time and money:
Ignoring wall thickness requirements
Minimum wall thickness for investment casting is typically 0.020" to 0.030" depending on alloy and size. Designing thinner walls creates casting defects and adds cost through rework or scrapping.
Skipping DFM review
Launching tooling without a thorough design-for-manufacturability review is expensive insurance to skip. A good DFM review catches thick sections, undrillable holes, and internal passage issues before they become expensive rework.
Requesting unrealistic tolerances
Investment casting as-cast tolerances are 0.005" per inch, not 0.001". Secondary machining can tighten this, but every 0.001" of additional tolerance adds cost and lead time. Understand what tolerances are truly critical.
Not budgeting for first article testing
Dimensional, hardness, chemical composition, and sometimes mechanical testing are standard. Budget 2 to 4 weeks and $2,000 to $10,000 for comprehensive FAT before production release.
Single-sourcing without a backup
Relying on a single investment caster with no backup creates supply chain risk. For critical parts, qualify a second source or ensure your tooling can be transferred to another facility.