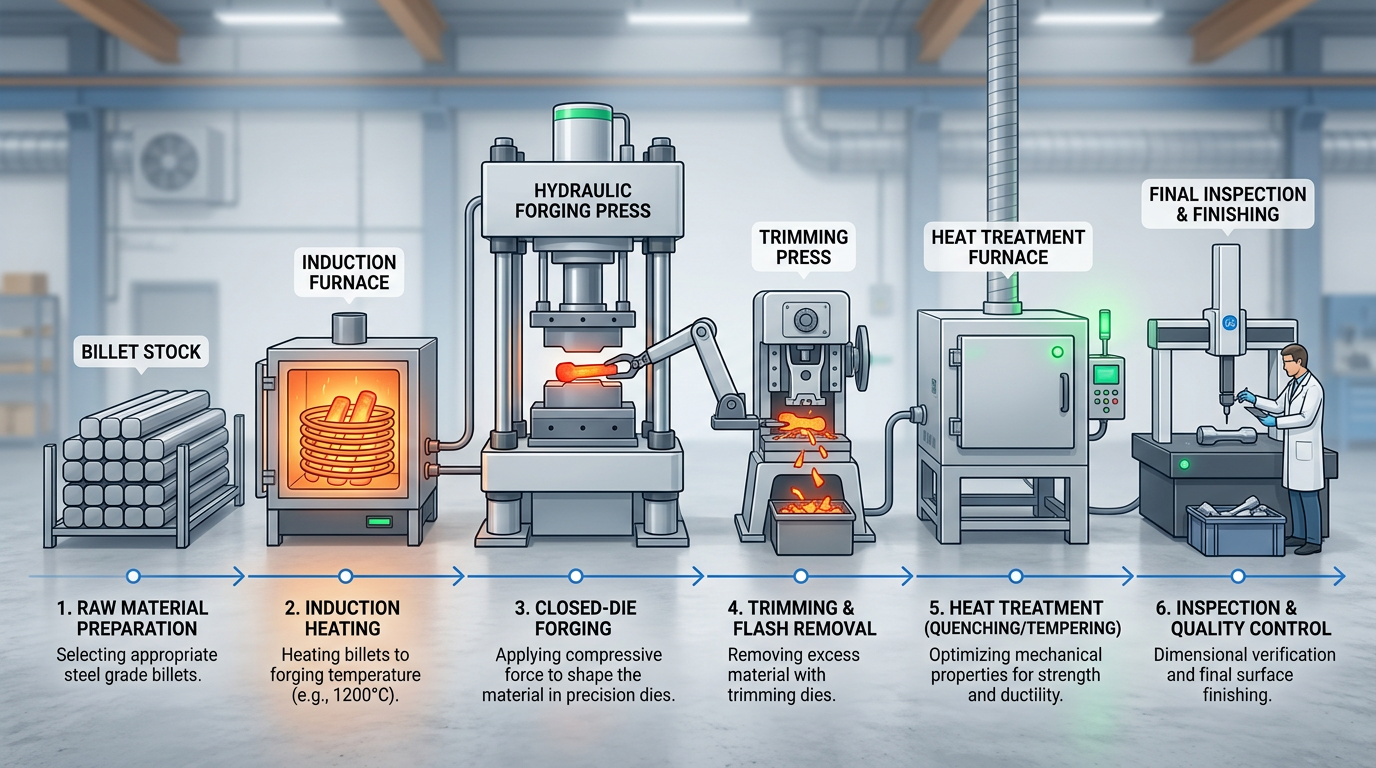
Contents
When to Use Forging
Forging is ideal when you need parts with superior strength, grain flow alignment, and durability. Understanding when forging is the right choice helps you make cost-effective manufacturing decisions.
High Strength Parts
When you need parts that can withstand extreme loads and stresses, forging produces superior grain flow alignment that cast or machined parts cannot match.
Critical Applications
Forged parts are essential for safety-critical components in aerospace, automotive, and industrial equipment where failure is not an option.
Medium to Large Production
Once tooling is established, forging becomes cost-effective for production runs of hundreds or thousands of parts with excellent repeatability.
Weight Reduction
Forged parts offer better strength-to-weight ratios than castings, making them ideal for aerospace and automotive applications where weight matters.
Forging Processes
Three primary forging methods dominate the industry, each with distinct advantages. Understanding the differences helps you select the best process for your part requirements and volume needs.
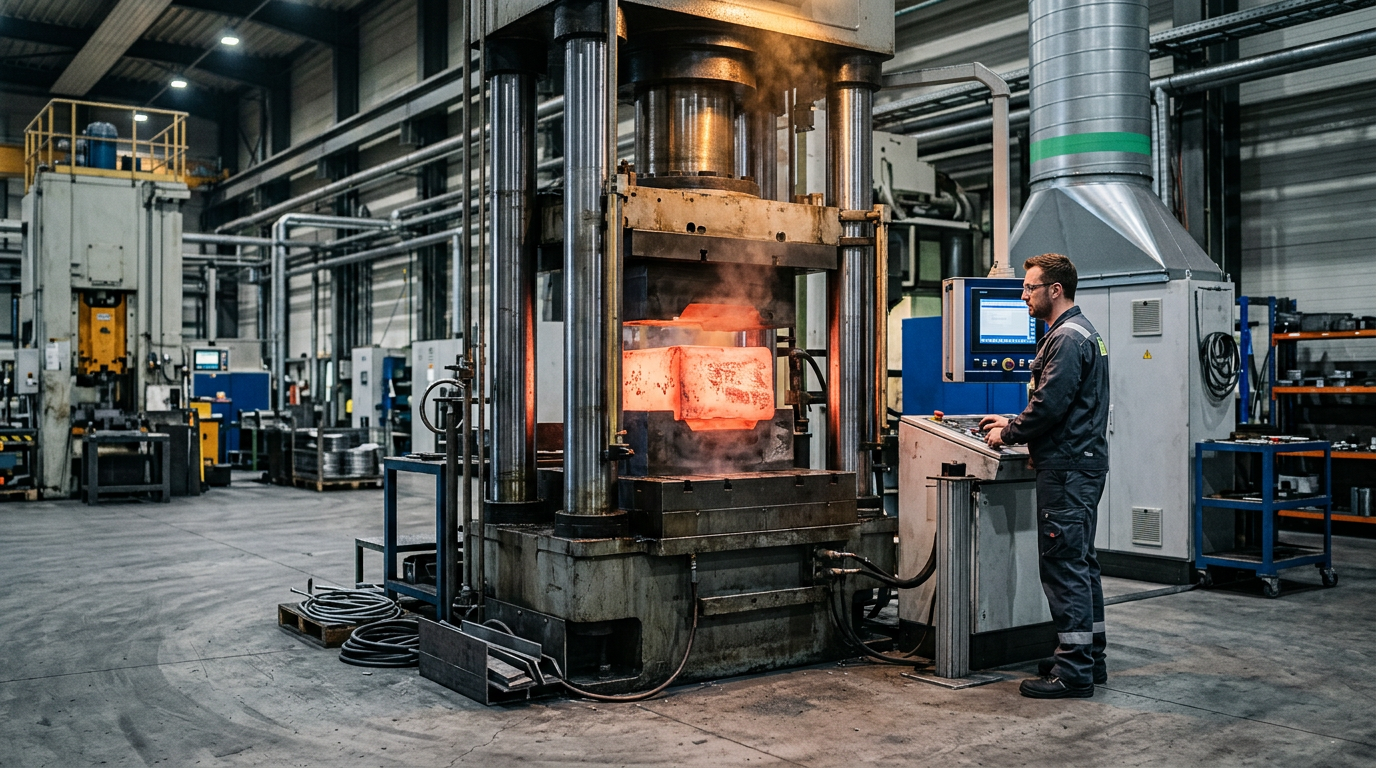
Open Die Forging
Uses simple flat or slightly shaped dies. Metal is shaped by multiple hammer or press strokes, allowing flexibility for custom geometries and sizes.
- Minimal tooling cost
- Flexible part design
- Large size capability
- Quick setup
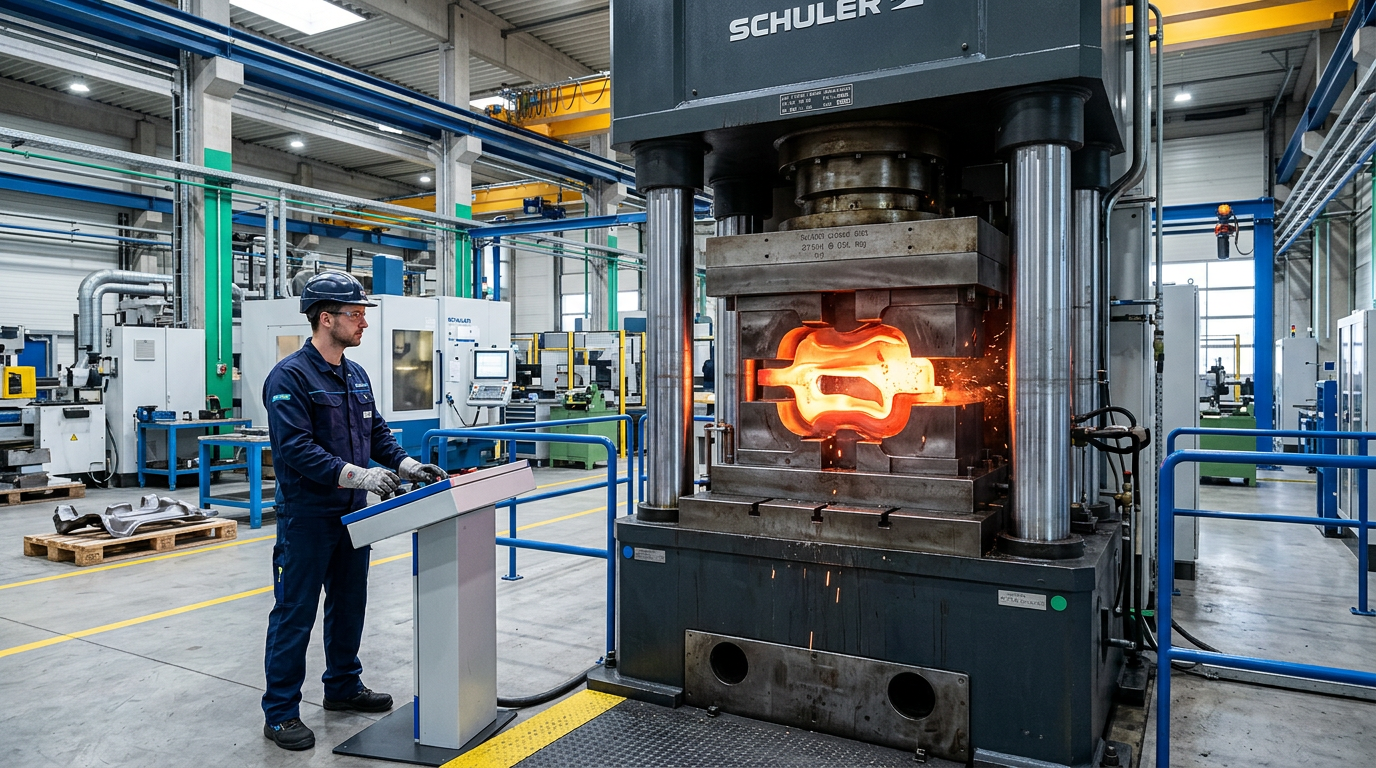
Closed Die Forging
Uses precisely shaped dies that form the part in a closed cavity. Produces near-net-shape parts with excellent dimensional accuracy and surface finish.
- Superior precision
- Better surface finish
- Less material waste
- Higher production rates
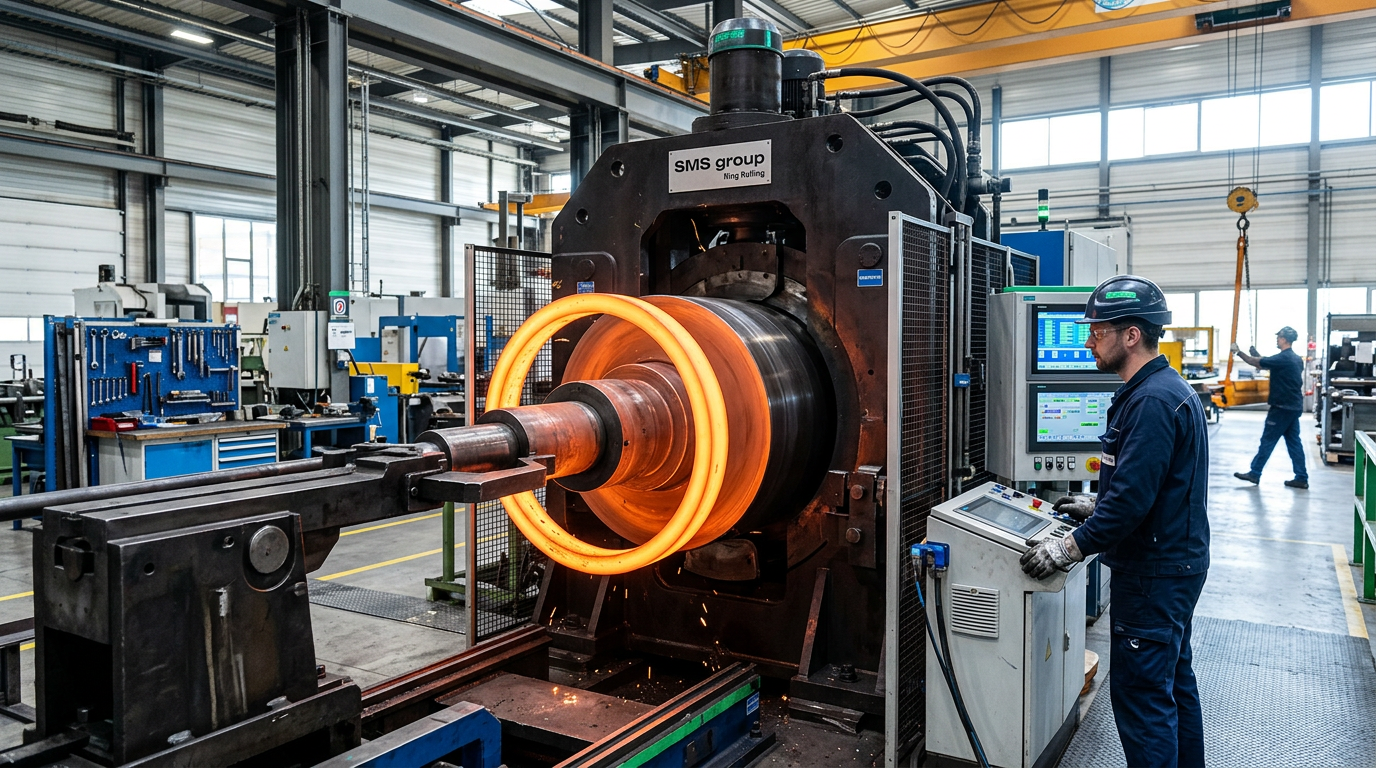
Ring Rolling
Specialized process for creating seamless rings and large diameter cylindrical parts. Metal is progressively shaped between rotating rolls.
- Seamless rings
- Excellent grain flow
- Large diameters
- High strength
Materials and Selection
Forging accommodates a wide range of materials, each offering different properties. Selecting the right material depends on your application requirements, operating temperatures, and corrosion resistance needs.
| Material | Properties | Typical Applications | Cost Level |
|---|---|---|---|
| Carbon Steel | High strength, good ductility, machinability | Connecting rods, crankshafts, hand tools | Low |
| Alloy Steel | Enhanced strength, wear resistance, toughness | Drive shafts, automotive components, industrial equipment | Medium |
| Stainless Steel | Corrosion resistance, aesthetic appeal, temperature resistance | Valves, medical implants, marine hardware | Medium-High |
| Aluminum | Lightweight, good strength-to-weight, excellent machinability | Aerospace components, automotive parts, industrial hardware | Medium |
| Titanium | Extreme strength, lightweight, high temperature resistance | Aerospace engines, medical devices, military applications | High |
| Superalloys | Exceptional high-temperature strength, oxidation resistance | Turbine blades, jet engines, extreme environment applications | Very High |
Note: Material selection should consider not only initial material cost but also machinability, heat treatment requirements, and final part performance characteristics.
Tooling and Die Costs
Die costs are a major consideration in forging projects. Understanding the factors that influence tooling investment and how to optimize die life helps you make better manufacturing decisions.
Die Development Process
-
1
Design and Engineering
Engineers analyze your part design, grain flow requirements, and production volume to create optimized die designs that balance cost and performance.
-
2
Die Material Selection
Die material choice depends on the forging material, production volume, and desired die life. Higher production volumes justify more expensive die steel.
-
3
Die Fabrication
Dies are machined and finished with precision. Complex dies with intricate features require more sophisticated machining and longer lead times.
-
4
Testing and Adjustments
Dies are tested with sample forgings. Adjustments and modifications are made to achieve desired dimensional accuracy and surface quality.
-
5
Production Readiness
Once dies are approved, they are ready for production runs. Proper maintenance during production extends die life and reduces unexpected replacements.
How to Evaluate Manufacturers
Choosing the right forging manufacturer is critical to your project's success. These key evaluation criteria will help you identify partners who can reliably deliver quality parts on time.
Equipment Capability
Verify they have press tonnage, furnace capacity, and specialized equipment needed for your part specifications and production volume.
Industry Experience
Look for manufacturers with proven experience in your industry vertical, whether aerospace, automotive, oil and gas, or industrial equipment.
Quality Certifications
Verify ISO 9001, AS9100, or industry-specific certifications. Request quality documentation and traceability systems.
Responsive Communication
Evaluate their responsiveness to initial inquiries, willingness to discuss your needs, and ability to provide clear quotes and timelines.
Customer References
Request and contact customer references. Ask about on-time delivery, quality performance, and willingness to support custom requirements.
Production Capacity
Ensure they have available capacity to meet your timeline and can scale production if your volume requirements increase.
RFQ Best Practices
Getting accurate quotes and establishing clear expectations requires providing detailed information to your potential suppliers. These best practices help you get competitive bids and avoid surprises.
1. Provide Complete Drawings
Include detailed 2D or 3D drawings with all dimensions, tolerances, surface finish requirements, and material specifications. Unclear drawings lead to inaccurate quotes.
2. Specify Volume Requirements
Clearly state your annual or lifetime volume requirements. Manufacturers adjust tooling investment and pricing based on expected production volumes.
3. Define Timeline Expectations
Communicate your required delivery dates and any time-sensitive constraints. Early engagement helps manufacturers plan their schedules accordingly.
4. Request Cost Breakdown
Ask for itemized quotes showing material costs, die costs, labor, and secondary operations. This transparency helps you understand pricing and identify optimization opportunities.
5. Discuss Secondary Operations
Clarify which operations are included (trimming, heat treatment, machining, inspection) and which are optional. Unnecessary secondary operations inflate costs.
6. Explore Cost Reduction Options
Ask manufacturers for recommendations on design changes that could reduce die costs, material waste, or production time. Collaborative engineering often yields significant savings.
Common Mistakes to Avoid
Learning from others' mistakes helps you avoid costly errors in your forging projects. These are the most common pitfalls and how to prevent them.
1. Underestimating Die Costs
Many projects fail because die costs exceed initial budgets. Always allocate 15-25% contingency for die adjustments and modifications during tooling validation.
2. Poor Communication of Specifications
Ambiguous drawings or incomplete specifications lead to scrap, rework, and disputes. Invest time in clear communication upfront to avoid expensive mistakes.
3. Selecting Based on Price Alone
The lowest quote often indicates the manufacturer hasn't fully understood your requirements. Balance price with quality, capacity, and reliability.
4. Ignoring Lead Times
Die fabrication and tooling validation require time. Plan projects with realistic lead times to avoid rush charges and quality compromises.
5. Neglecting Grain Flow Considerations
Not optimizing part design for grain flow alignment wastes the benefits of forging. Collaborate with manufacturers on grain flow direction for maximum part performance.