
1. When to Use CNC Machining (and When Not To)
CNC machining is one of the most versatile manufacturing processes for producing precise metal and plastic components at medium and high volumes. However, it is not the right fit for every application. Understanding when CNC machining excels will help you make informed sourcing decisions and avoid costly mistakes.
Tight Tolerances
CNC machining achieves repeatable precision far better than casting or forming. Standard CNC tolerances of plus or minus 0.005 inches are common, with tighter tolerances down to plus or minus 0.001 inch achievable with advanced equipment and careful setup. For applications where dimensional accuracy is critical, CNC machining is the right choice.
Complex Geometries
CNC machines excel at creating complex shapes, holes, pockets, threads, and contours that would be difficult or impossible with casting or forming. From intricate aerospace components to precision medical devices, CNC can machine any geometry you can design.
Material Flexibility
CNC machines work with virtually any machinable material including aluminum, steel, stainless steel, titanium, plastics, and composites. This flexibility allows you to select the optimal material for your application without being limited by manufacturing process constraints.
No Tooling Constraints
Unlike die casting or injection molding, CNC machining requires no custom tooling. You can machine prototype quantities and low volumes as economically as high volumes. Program once, machine as many or as few parts as you need at any time.
When to consider other processes
If you need extremely high volumes (above 50,000 pieces per year) of simple parts, injection molding or die casting may offer lower per-unit costs. For very large parts exceeding machine capacity, forging or welded fabrication may be better. For very soft or elastic materials, other forming methods may be more suitable.
2. Understanding the Main Machining Processes
CNC machining encompasses several distinct processes, each with different capabilities and best applications. Understanding how each process works helps you select the right technology for your parts.
CNC Milling
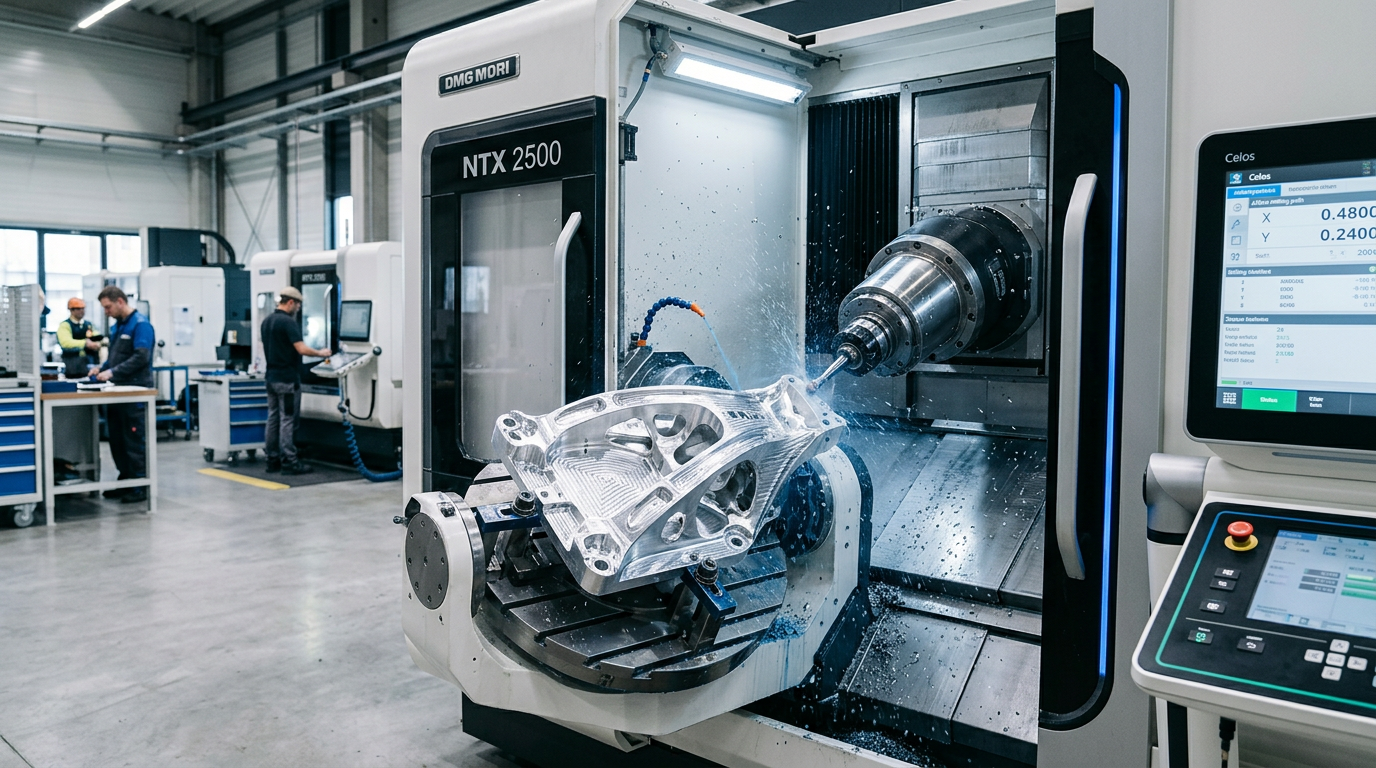
Milling uses rotating cutting tools to remove material from a stationary part. Multiple tools can work on different faces and axes. 3-axis mills are most common, while 4-axis and 5-axis machines enable complex 3D geometries and angled surfaces without repositioning.
- Tool types: End mills, drills, face mills, taps
- Axes: 3-axis, 4-axis, and 5-axis available
- Tolerance: plus or minus 0.005 to 0.001 inches
- Speed: Medium production rates, good flexibility
- Best for: Complex shapes, pockets, slots, holes, general work
CNC Turning
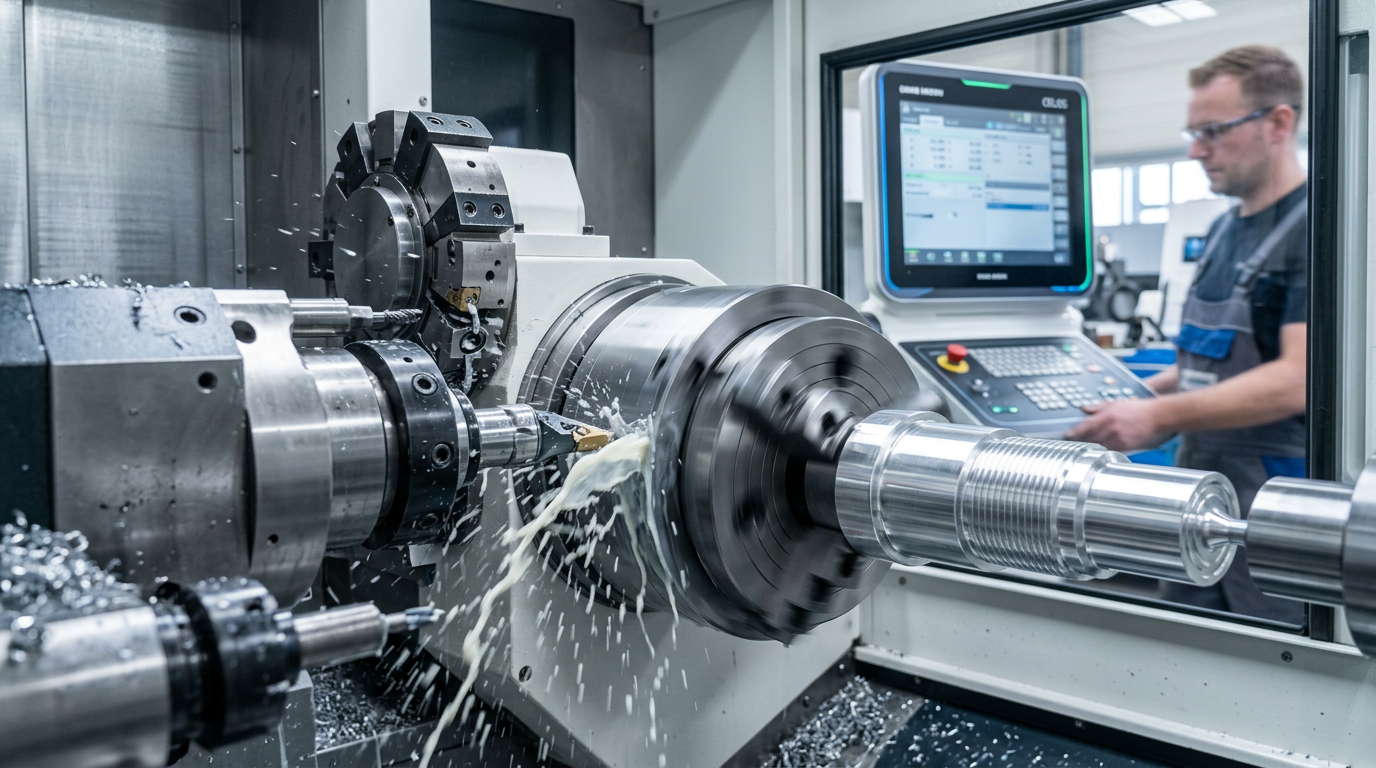
Turning rotates the part against stationary cutting tools. The lathe removes material as the part spins, creating cylindrical and tapered shapes. CNC turning is extremely fast and efficient for round parts, shafts, and bushings with excellent accuracy.
- Tool types: Turning tools, threading tools, boring bars
- Axes: Typically 2-axis (diameter and length)
- Tolerance: plus or minus 0.003 to 0.001 inches
- Speed: Fastest production rates, highly efficient
- Best for: Cylindrical parts, shafts, bushings, rotational components
Swiss Machining
Swiss machines combine features of lathes and mills, with the cutting tool and part moving on multiple axes simultaneously. This allows extreme precision and multiple operations in a single setup. Swiss machines are optimized for small to medium parts with tight tolerances and complex geometries.
- Tool types: Similar to lathes but with multiple simultaneous operations
- Axes: 3 to 5+ axes with coordinated motion
- Tolerance: plus or minus 0.0005 to 0.0001 inches achievable
- Speed: Extremely fast for complex small parts
- Best for: Medical devices, watch components, electronic parts, extreme precision requirements
- Typical parts: Under 2 inches long with multiple features, minimal secondary operations needed
Pro tip
Discuss your part design with potential manufacturers before finalizing your drawings. A skilled machinist can suggest design changes that reduce setup time, improve tolerances, or eliminate secondary operations. Engaging the manufacturer early in design often saves thousands in production costs.
3. Materials and Machining Capabilities
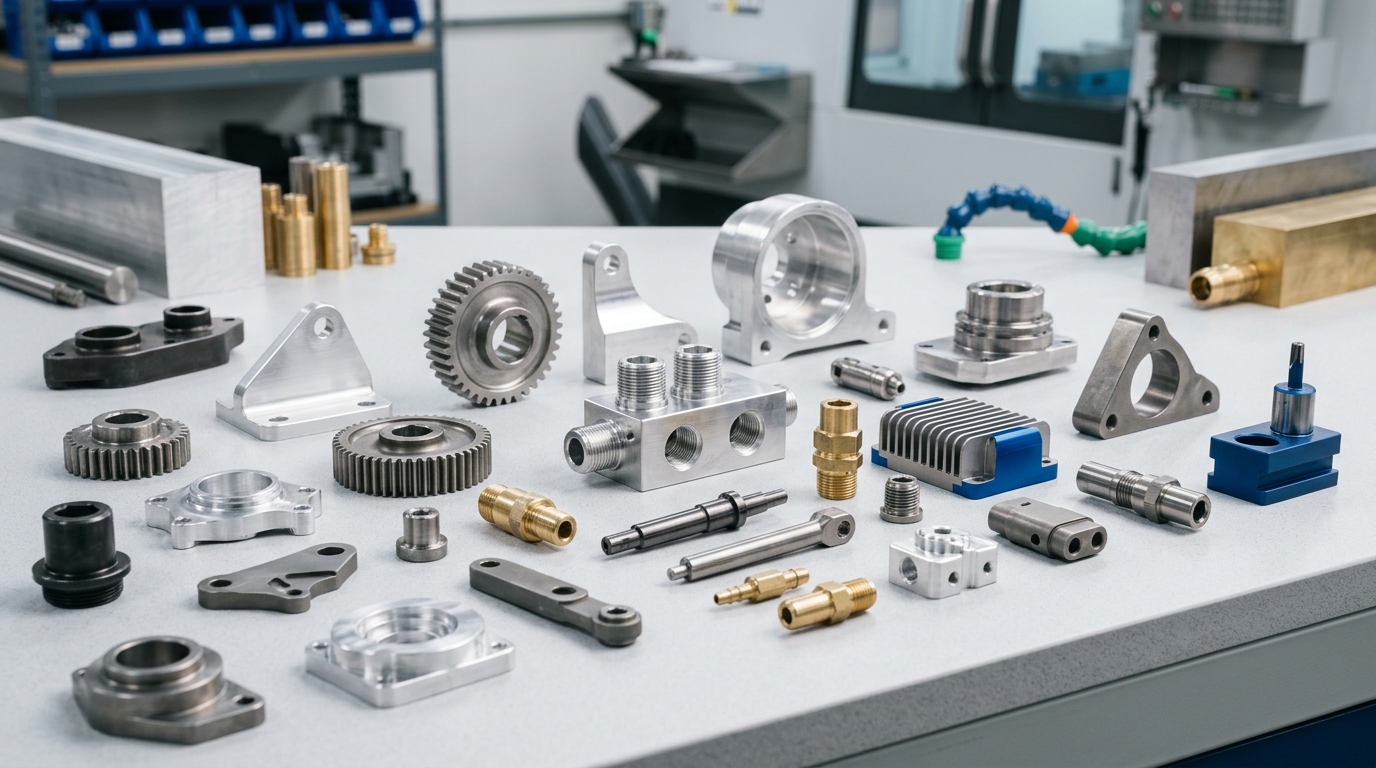
CNC machines can work with virtually any machinable material. Material selection dramatically affects part cost, performance, and lead time. Here is a guide to the most common materials and their machining characteristics:
| Material | Machinability | Cost | Best Applications |
|---|---|---|---|
| Aluminum | Excellent | Low | Aerospace, automotive, consumer products, lightweight applications |
| Mild Steel | Good | Low | General machinery, structural parts, brackets, industrial equipment |
| Stainless Steel | Fair | Medium | Medical devices, food processing, marine environments, corrosion-critical applications |
| Titanium | Fair | High | Aerospace, military, medical implants, high-performance applications |
| Plastics | Excellent | Low-Medium | Consumer products, prototypes, housings, insulators, light-duty applications |
Pro tip
Aluminum and plastics are the fastest and least expensive to machine, offering per-hour rates around $50 to $75. Steel runs $75 to $125 per hour due to harder tool life. Stainless steel and titanium can exceed $300 per hour due to heat generation, tool wear, and specialized coolant requirements. Discuss material costs with your manufacturer before finalizing specifications.
4. Understanding Setup and Programming Costs
Unlike die casting or injection molding, CNC machining has no custom tooling cost. However, setup, programming, and first-piece verification represent significant costs for each part number. Understanding these costs helps you budget accurately and optimize your production strategy.
Programming and CAM setup
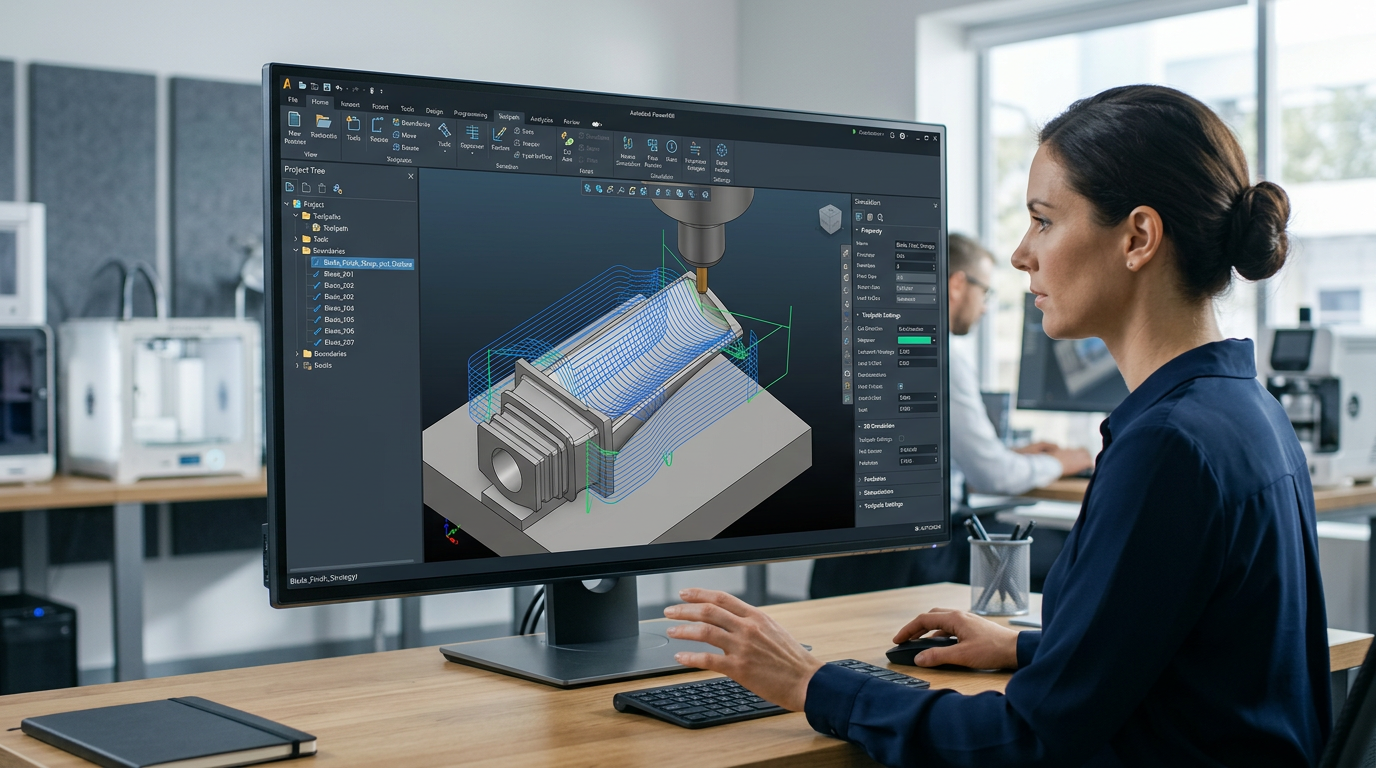
A programmer must convert your CAD file into machine code, selecting tool paths, feeds, speeds, and tool changes. Simple parts require 1 to 2 hours ($200 to $400). Complex multi-axis parts may require 10 to 40 hours ($2,000 to $8,000) for optimized toolpaths. Programs are reusable for all subsequent parts, so setup cost distributes across your total order.
Machine time and hourly rates
Machine rates vary by machine type and facility location. A basic 3-axis mill runs $50 to $100 per hour. 5-axis simultaneous mills run $150 to $250 per hour. CNC turning is typically $40 to $80 per hour. Swiss machines run $100 to $200 per hour. Your total piece cost depends directly on machine hours, so efficiency directly impacts pricing.
Fixturing and work-holding
Standard vises and chuck jaws work for many parts. Complex parts or high volumes may require custom fixtures to speed setup and reduce cycle time. A custom fixture costs $500 to $5,000 depending on complexity, but amortizes quickly on large orders by reducing setup time on each run.
Tolerances and quality control
Standard tolerances (plus or minus 0.005 inches) use basic setup and in-process checking. Tight tolerances (plus or minus 0.002 to 0.001 inches) require more careful setup, frequent measurement with precision instruments, and sometimes tool compensation adjustments. Extremely tight tolerances (plus or minus 0.0005 inches) may require SPC statistical control and add 20 to 50 percent to labor cost.
Material waste and scrap
CNC machining removes material to create the part, generating chips and scrap. Simple parts may waste 10 to 20 percent of material. Complex parts requiring heavy machining can waste 50 to 80 percent of raw material. Material cost is quoted at the full input weight, so material efficiency directly affects cost. Discuss design optimization with your manufacturer to minimize waste.
Pro tip
Batch orders to spread programming and setup costs across more parts. An order for 100 parts is often less than double the per-unit cost of 50 parts because programming and setup costs are shared. If you anticipate needing parts later, ordering in larger quantities upfront typically saves money even if you carry inventory.
5. How to Evaluate a CNC Manufacturer
Choosing the right CNC manufacturer affects your quality, costs, reliability, and long-term product success. Request a facility tour and evaluate manufacturers on these critical dimensions:
Equipment Capabilities
What machine types and axis counts do they have? CNC mills (3, 4, or 5-axis), turning centers, and Swiss machines? Can they handle your part size? Can they achieve your required tolerances? Ask to see the equipment list with model numbers and specifications.
Quality Certifications
ISO 9001 demonstrates commitment to quality management systems. AS9100 (aerospace), ITAR (military), or medical device certifications verify capability for regulated industries. Ask for certificate of compliance with your required standards and speak to their quality manager about in-process controls.
Material Experience
Do they specialize in your required materials? Aluminum machines differ from steel, and exotic materials like titanium require specialized expertise. Ask about experience with similar materials and review their material library. Manufacturers with deep expertise deliver better results.
Production Capacity
How many machines do they operate? What is their current utilization? Can they meet your delivery timeline? During facility tour, observe work-in-process inventory and scheduling board to assess realistic capacity and lead times. A manufacturer at 90+ percent utilization may promise 4 weeks but deliver in 8.
Engineering and Design Support
Do they offer design-for-manufacturability feedback? Can they suggest design changes to reduce costs? Will they optimize your CAD for better machine efficiency? A manufacturer willing to invest time in design review upfront often delivers lower costs and better results than one who simply quotes your drawings as-is.
Communication and Responsiveness
How quickly do they respond to inquiries? Do you have a dedicated project manager? How do they handle problems or engineering changes? Reliable communication is as important as machining skill. A manufacturer responsive to your questions will be responsive to problems.
Request sample parts from manufacturers you are seriously considering. Compare the quality and surface finish. Schedule a facility visit before committing to major orders. Seeing the equipment, work culture, and operational discipline in person reveals far more than a website or brochure ever could.
6. Creating an Effective RFQ
A well-structured RFQ gets you faster responses, better quotes, and more accurate pricing. Include all critical information so suppliers can provide comprehensive cost estimates and timeline projections without multiple follow-up questions:
3D CAD File
STEP or IGES format with all critical dimensions and features clearly defined
2D Drawing with GD&T
Geometric dimensioning and tolerancing, surface finish callouts, and material specification
Material Requirements
Material grade (aluminum 6061-T6, stainless 316, etc.), hardness, and any special material certs required
Annual Volume
Expected annual quantity and planned release schedule over 3 to 5 years
Secondary Operations
Deburring, heat treatment, plating, anodizing, painting, assembly, testing requirements
Quality Standards
Required certifications, inspection level, material testing, and reporting expectations
Pro tip
Send your RFQ to 3 to 5 qualified manufacturers. Fewer than 3 does not provide sufficient pricing comparison. More than 5 creates confusion and dilutes individual attention. Request quotes broken down by machine time, programming, fixtures, and material so you can compare apples to apples and identify cost drivers.
7. Common Mistakes CNC Machining Buyers Make
After years of working with manufacturing buyers, we see the same sourcing mistakes repeated. Learn from these common pitfalls and avoid the costly consequences:
Specifying tighter tolerances than needed
Every 0.001 inch of tolerance reduction significantly increases cost. Standard tolerances of plus or minus 0.005 inches are usually sufficient. Before finalizing specifications, verify from your design and assembly engineering what tolerances your application truly requires. Unnecessary tightness drives unnecessary costs.
Designing features that are difficult to machine
Sharp internal corners require special tools and extra passes. Deep narrow pockets require long tools that deflect and chatter. Thin walls require careful feeds and speeds to avoid breakage. Undercuts that can't be machined in one setup create secondary operation costs. Discuss your design with a manufacturer before finalizing drawings to catch manufacturability issues.
Choosing based on price alone
The lowest quote often reflects lower quality, longer lead times, or hidden cost adjustments later. A manufacturer offering 30 percent below market is likely cutting corners or planning to offset costs through change orders. Evaluate the total value: quality, reliability, communication, and long-term partnership potential.
Not discussing design optimization upfront
A skilled machinist can often suggest design changes that dramatically reduce cost without affecting function. Rounding a corner slightly reduces tooling time. Moving a hole location simplifies fixturing. Eliminating an undercut eliminates a secondary operation. These conversations should happen during quoting, not after tooling is already in place.
Single-sourcing without understanding capacity limits
Relying on one manufacturer creates vulnerability if they experience equipment failure, capacity constraints, or quality problems. For critical parts, develop a qualified second source or ensure your documentation is portable so another manufacturer can quickly take over if needed.